Shops weighing how to produce threads inside bores have a flexible alternative to tapping. The process synchronizes Z axis feed with spindle rotation, accommodates varied thread standards, pitches and difficult materials, and is often the preferred route for large diameters, interrupted bores and short runouts where torque and chip packing make taps unreliable. Success rests on geometry, kinematics, rigidity, chip formation, programming strategy and inspection.
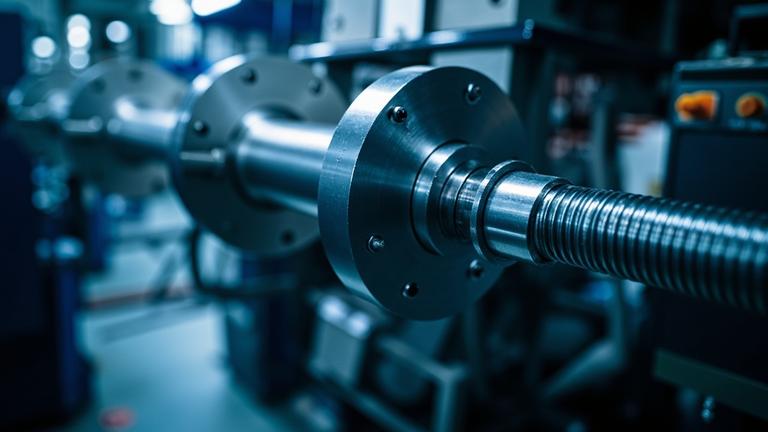
Internal thread turning cuts a helical thread form inside a bore, with the Z axis feed synchronized to spindle rotation.
What the process does
Internal thread turning is the process of generating a helical thread form inside a bore. The mechanics hinge on synchronization: the Z axis feed moves in step with spindle rotation, producing the thread helix as a machined cut rather than a formed or tapped feature.
That single kinematic relationship is what gives the process its range. Because the thread form is generated by a toolpath rather than dictated by a fixed tool, the same basic approach adapts to work that would otherwise demand dedicated tooling for each job.
Where it beats tapping
Compared with tapping, internal thread turning offers superior flexibility. It handles thread standards, variable pitches, and difficult materials without locking the shop into a tap for every combination.
It is often the preferred method for large diameters, interrupted bores, and short thread runouts. It is also the fallback when torque and chip packing make taps unreliable, the failure modes that turn a routine threading operation into scrap risk and machine downtime.
The fundamentals that decide success
The technical fundamentals that determine success in internal thread turning are geometry, kinematics, rigidity, chip formation, programming strategy, and inspection. Each one carries weight. Rigidity and chip formation govern whether the cut stays stable inside the bore. Geometry and kinematics govern whether the thread form is correct. Programming strategy and inspection govern whether the process repeats from part to part.
Shops that treat threading as a tooling purchase miss the point. This is a process capability, and it is built across all of those fundamentals together.
- For quoting: a process that spans thread standards, variable pitches, and difficult materials lets a shop bid a wider range of threaded-bore work without new tooling for every job.
- For process planning: large diameters, interrupted bores, and short runouts are the parts where taps become a liability. That is where thread turning earns its place on the route sheet.
- For capability: the differentiators are geometry, kinematics, rigidity, chip formation, programming strategy, and inspection. Invest there before blaming the tool.
Read the full article on Scandinavian Tool Systems AB
Is this your company?
This article features your business. Claim it to add your logo, contact details, and a link to your website — or upgrade to reach more buyers.
Did you know 80% of Press Releases trigger AI content warnings? Reach out and the M4S team can assist.